Can High Initial Bond PUR Lamination Glue Stop Film Shifting and Rebound on High-Speed Furniture Lamination Lines?
On a high-speed furniture panel lamination line, a film does not have to completely delaminate to create a production problem.
Sometimes the problem starts much earlier.
The PET or PVC film looks properly positioned immediately after lamination, but as the laminated panel moves through conveying, trimming, cutting, stacking, or the next machining process, the film begins to move back toward its original position. Corners may lift slightly. The film may shift several millimeters. A small alignment error becomes a visible defect after trimming.
For a panel lamination factory running continuously, this can quickly turn into:
Film Rebound → Film Shifting → Cutting Error → Defective Panel → Rework → Line Downtime
The underlying problem may not be the film itself.
In many cases, the production line needs an adhesive with enough initial bonding strength to hold the film securely during the critical period immediately after lamination.
This is where High Initial Bond PUR Lamination Glue becomes an important option for high-speed furniture lamination.
For manufacturers processing PET, PVC, acrylic, and other decorative films, the procurement question is not simply whether a PUR adhesive can achieve strong final bonding.
The more practical question is:
Can the adhesive provide enough initial hold to keep the film accurately positioned before the next high-speed production process begins?
1. User Problem: Why Does Film Rebound or Shift After Lamination?
High-speed lamination lines are designed to keep material moving.
The laminated panel may quickly enter:
Conveyor systems
Cutting equipment
Trimming units
Stacking systems
Edge-processing equipment
Packaging lines
This creates a narrow window between lamination and downstream processing.
If the adhesive has insufficient initial bonding strength, the film may still have a tendency to move while the adhesive is developing its final strength.
Typical Symptoms
Furniture panel manufacturers may notice:
PET film shifting after lamination
PVC film moving during conveying
Film edges lifting
Film rebound after pressing
Misalignment during cutting
Film wrinkles near panel edges
Uneven decorative patterns
Increased trimming defects
Repeated manual correction
Production-line stoppages
The problem becomes particularly obvious with films that have a strong tendency to recover their original shape after being pressed or formed.
Why Does Film Rebound Happen?
Decorative films can contain internal stresses created during manufacturing, handling, heating, stretching, or forming.
After the film is laminated onto a substrate, these forces may continue to act on the adhesive interface.
If the adhesive's initial green strength is insufficient, the film can partially recover before the bond has developed enough resistance.
The result is what operators often describe simply as:
“The film keeps bouncing back.”
However, the technical issue is more accurately described as a mismatch between:
Film Recovery Force + Line Speed + Initial Adhesive Strength + Pressure/Contact Time
This is why simply increasing the amount of ordinary PUR glue may not solve the problem.
| Symptom | Possible Cause | What to Check |
|---|---|---|
| PET film shifts after conveying | Insufficient initial bond | Initial bonding strength |
| Film rebounds at edges | Film memory + weak early hold | Film tension + adhesive |
| Film moves during cutting | Bond not stable enough before cutting | Initial bonding + line speed |
| Uneven glue line | Viscosity/coating issue | Temperature + coating amount |
| Good initial hold but later delamination | Final curing/bond issue | Moisture + curing + substrate |
| High glue consumption | Excessive coating | Application amount + roller setting |
2. Product Selection: Why Consider High Initial Bond PUR Lamination Glue?
Traditional PUR lamination adhesives can provide strong final bonding after curing, but different formulations can behave very differently during the early stage of production.
For a high-speed lamination line, initial bonding strength deserves to be evaluated separately from final bond strength.
Initial Bond vs. Final Bond
Think of the bonding process as two stages.
Stage 1 — Immediate Positioning
The adhesive needs to hold the film firmly enough to resist:
Film rebound
Conveyor vibration
Mechanical movement
Trimming forces
Handling
Stage 2 — Long-Term Bond Development
The adhesive continues to develop its final bonding performance and resistance to:
Heat
Moisture
Aging
Chemicals
Environmental changes
A good PUR lamination adhesive for high speed line therefore needs to balance both stages.
High initial strength without sufficient long-term performance is not enough.
Likewise, excellent final adhesion is not enough if the film shifts before the next production process.
What Makes Tonren's High Initial Bond PUR Lamination Glue Different?
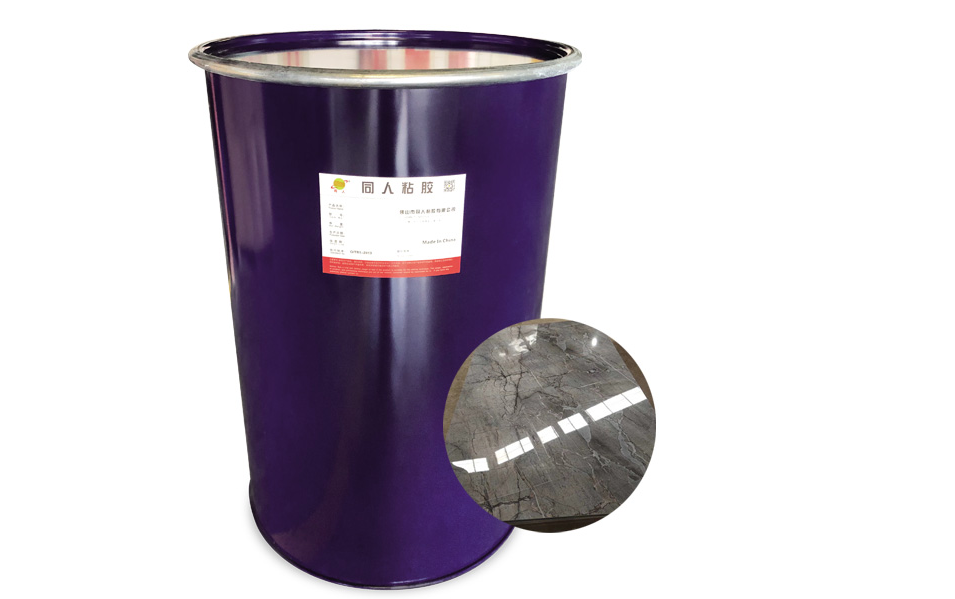
Foshan Tonren Adhesive Co., Ltd offers a High Initial Bond PUR Lamination Glue developed for flat lamination applications where early bonding performance is particularly important.
Tonren's published product information identifies:
8131 as a universal PUR type with excellent leveling properties, especially suitable for high-gloss film lamination.
8133 as a PUR type with better initial bonding strength, suitable for thicker decorative film lamination.
The listed application materials include PVC high-gloss film, acrylic, transparent PET, and other surface materials.
This makes the product family particularly relevant when a furniture panel manufacturer is balancing:
High-Speed Production + Film Positioning + Surface Quality + Long-Term Bonding
3. Technical Parameters: What Should High-Speed Lamination Buyers Check?
A procurement team should not choose a PUR lamination adhesive only because its product name contains “high initial bond.”
The technical parameters need to match the production line.
3.1 Initial Bonding Strength
This should be one of the first evaluation items for a high-speed line.
Ask the supplier:
How quickly does the adhesive develop initial strength?
What is the test method?
What substrates were used?
What film was used?
How long after lamination was the bond evaluated?
A useful production trial should measure film movement during the actual interval between lamination and downstream processing.
3.2 Viscosity
Viscosity influences:
Adhesive transfer
Roller coating
Glue distribution
Coating uniformity
Machine stability
Required operating temperature
Tonren's published information lists the following specifications:
| Product | Type | Viscosity | Recommended Operating Temperature | Main Feature |
|---|---|---|---|---|
| 8131 | PUR | 6,000 ± 1,000 mPa·s at 130°C | 110–140°C | Universal type, excellent leveling |
| 8133 | PUR | 12,000 ± 2,000 mPa·s at 130°C | 120–150°C | Higher initial bonding strength |
These are manufacturer-published reference specifications; buyers should confirm the current TDS and recommended settings before production use.
3.3 Application Temperature
Temperature affects adhesive viscosity and coating behavior.
If the operating temperature is too low:
Adhesive may not flow correctly
Wetting may become inconsistent
Coating may become uneven
If the temperature is too high or the adhesive experiences excessive thermal exposure:
Viscosity can change
Processing stability can be affected
Adhesive residence time becomes more important
Therefore, the correct operating window should be established according to:
Adhesive + Machine + Substrate + Film + Production Speed
Tonren currently lists 110–140°C for 8131 and 120–150°C for 8133.
3.4 Leveling and Surface Quality
High-speed furniture lamination is not only about bonding.
The finished surface may be:
High gloss
Matte
Decorative
Transparent
Textured
Poor adhesive leveling can contribute to visible surface defects, especially on reflective films.
For this reason, buyers should evaluate:
Initial Bond + Leveling + Surface Appearance
rather than initial bond alone.
Tonren specifically describes 8131 as having excellent leveling properties and notes its suitability for high-gloss film lamination.
3.5 Coating Amount
More glue does not automatically mean better initial bonding.
Excessive adhesive can increase:
Material consumption
Production cost
Surface defects
Cleaning requirements
Potential squeeze-out
Insufficient adhesive can create:
Weak wetting
Local bonding failure
Film lifting
Uneven adhesion
The objective should be:
Minimum Effective Coating Amount + Uniform Coverage + Sufficient Initial Bond
The optimum coating amount should be confirmed through an actual production trial.
3.6 Open Time
Open time needs to match the equipment and production process.
For high-speed lines, an adhesive with a suitable working window allows the manufacturer to maintain stable coating and bonding while avoiding unnecessary delays.
But “shorter” is not automatically better.
The correct open-time profile depends on:
Line speed
Film type
Substrate temperature
Adhesive temperature
Pressing conditions
Contact time
Therefore, buyers should evaluate open time together with initial strength rather than using either parameter independently.
4. Application Scenarios: Where Is High Initial Bond PUR Especially Useful?
4.1 PET Film Lamination
PET decorative films can be used for high-end furniture panels, cabinets, doors, and decorative surfaces.
Because of the film's mechanical characteristics and appearance requirements, stable positioning is important.
A suitable furniture film lamination glue should provide sufficient initial hold while maintaining long-term adhesion.
4.2 PVC Decorative Film Lamination
PVC remains widely used for furniture and interior decorative panels.
Applications may include:
Cabinet doors
Wall panels
Furniture boards
Decorative panels
Interior components
For high-speed production, the adhesive must maintain stable bonding while the panel moves quickly through downstream processes.
4.3 High-Gloss Furniture Panels
High-gloss surfaces make bonding defects particularly easy to see.
A suitable adhesive needs to provide:
Good wetting
Stable coating
Smooth leveling
Reliable initial bonding
Long-term adhesion
Tonren's 8131 is specifically described as having excellent leveling properties and being suitable for high-gloss film lamination.
4.4 Thick Decorative Films
Thicker films can create different bonding requirements from thin decorative films.
Tonren identifies 8133 as a higher-initial-bond formulation suitable for thick decorative film lamination.
For buyers processing thicker PET, PVC, or similar decorative layers, this type of formulation may deserve a direct production trial.
4.5 High-Speed Continuous Lamination Lines
The faster the line operates, the less tolerance there is for unstable initial bonding.
If a panel is immediately transferred to cutting or trimming after lamination, the adhesive needs to hold the film sufficiently during that transition.
This is why a PUR lamination adhesive for high speed line should be evaluated under the actual line speed rather than only through laboratory bonding tests.
5. Procurement Decision: How Should a Factory Compare PUR Lamination Adhesives?
A common purchasing mistake is to compare adhesives only by:
Price/kg
For high-speed lamination, a better calculation is:
Total Adhesive Cost = Adhesive Consumption + Film Waste + Rework + Downtime + Cleaning + Quality Loss
A slightly higher adhesive price may still be commercially attractive if it helps prevent repeated film-shifting defects.
Procurement Checklist
Before approving a new adhesive, ask:
1. What is the initial bonding strength?
Request the actual test conditions.
2. What films have been tested?
PET, PVC, acrylic, and other films may have different bonding requirements.
3. What substrates have been tested?
Consider MDF, particleboard, plywood, melamine boards, and other substrates used by your factory.
4. What is the recommended processing temperature?
Make sure it matches the machine's operating capability.
5. What is the viscosity at the recommended temperature?
This affects coating equipment compatibility.
6. What coating amount is recommended?
Compare performance and consumption together.
7. How quickly can the laminated panel enter the next process?
This is particularly important for high-speed production.
8. What final heat and moisture resistance can be expected?
Initial strength is only one part of the bonding system.
9. Can the supplier provide samples?
Actual machine testing should come before bulk approval.
10. Can the supplier provide technical support?
If film rebound continues, the root cause may involve the adhesive, film tension, coating amount, pressure, temperature, or machine speed.
6. How to Diagnose Film Shifting Before Changing the Adhesive
Not every film-shifting problem is caused by insufficient adhesive strength.
A professional troubleshooting process should check the complete system.
Film Side
Check:
Film thickness
Film stiffness
Surface treatment
Internal stress
Roll storage condition
Substrate Side
Check:
Surface cleanliness
Flatness
Dust
Moisture
Surface energy
Adhesive Side
Check:
Adhesive type
Initial bond
Viscosity
Temperature
Coating amount
Storage condition
Machine Side
Check:
Roller pressure
Line speed
Heating temperature
Pressing time
Conveyor transition
Film tension
Process Side
Check:
Coating → Lamination → Pressure → Initial Holding → Conveying → Cutting
This diagnostic chain helps identify whether the adhesive is actually the bottleneck.
7. Factory Solution: Why Work With Foshan Tonren Adhesive Co., Ltd?
For a furniture panel factory, changing adhesive can affect the entire production process.
This is why supplier technical support matters.
Foshan Tonren Adhesive Co., Ltd has more than 26 years of experience in adhesive R&D, manufacturing, and market service.
The company provides functional adhesive solutions for woodworking and furniture applications, including:
Edge Banding Adhesive
Wrap Glue
Lamination Glue
3D Lamination Glue
Solid Wood Glue
PUR Adhesive
Tonren's High Initial Bond PUR Lamination Glue product line is designed for flat lamination applications where strong early bonding and reliable final adhesion are important.
The published product information also states that the adhesive offers water, solvent, and heat resistance and can be used for PVC high-gloss film, acrylic, transparent PET, and other surface materials.
For buyers, this means the evaluation can focus on the actual production requirement rather than selecting a generic PUR adhesive from a catalogue.
8. Tonren's High Initial Bond Approach: Hold First, Cure Further
The key production objective is not simply to make the adhesive reach its final strength as quickly as possible.
The process needs to work in two stages.
Stage 1: Immediate Positioning
After the film contacts the adhesive-coated substrate, the adhesive should develop sufficient initial bonding to help resist:
Film rebound
Film shifting
Conveyor vibration
Handling
Cutting movement
Stage 2: Long-Term Bond Development
The PUR system then continues to develop its final bond performance.
The finished laminate needs to maintain reliable adhesion under the expected:
Temperature
Humidity
Water exposure
Aging
Service conditions
This balance is particularly important for furniture panels that must pass through multiple processes shortly after lamination.
9. How Should a Factory Test High Initial Bond PUR Lamination Glue?
A simple sample test can be designed around the actual production problem.
Test 1 — Standard Production Trial
Run the new adhesive on the existing machine using the normal:
Line speed
Temperature
Coating amount
Pressure
Film
Substrate
Test 2 — Immediate Position Stability
Check the laminated film immediately after:
Conveying
Turning
Trimming
Cutting
Record whether the film moves relative to the substrate.
Test 3 — Rebound Observation
Observe whether the film edges or corners attempt to return to their original shape after pressing.
Test 4 — Appearance Inspection
Check:
Surface smoothness
Wrinkles
Bubbles
Glue-line visibility
Film alignment
Test 5 — Final Bond Evaluation
After sufficient curing, evaluate:
Peel behavior
Adhesion
Heat resistance
Moisture resistance
Other application-specific requirements
This provides a much more useful purchasing result than simply testing whether two materials can be bonded together.
10. High Initial Bond Does Not Mean “More Glue”
One common misunderstanding is that higher initial bonding can simply be achieved by increasing adhesive consumption.
This is not a reliable production strategy.
If the coating amount is excessive, the factory may experience:
Higher adhesive costs
Uneven coating
Squeeze-out
Surface contamination
Longer cleaning intervals
The objective of a high-performance lamination adhesive is to obtain sufficient bonding performance at a controlled application amount.
Therefore, the correct optimization target is:
Adhesive Formulation + Coating Amount + Temperature + Pressure + Line Speed
not simply:
More Glue = More Bonding
11. FAQ: High Initial Bond PUR Lamination Glue
Can High Initial Bond PUR Lamination Glue stop PET film from shifting?
It can help reduce film shifting when insufficient initial adhesive strength is a contributing factor. However, film tension, substrate condition, coating amount, pressure, machine speed, and other process variables must also be controlled.
Why does PET or PVC film rebound after lamination?
Possible causes include film internal stress, insufficient initial bonding, unsuitable adhesive viscosity, insufficient coating, inadequate pressure, or excessive line speed. A complete process diagnosis is recommended before changing the adhesive.
Is high initial bond more important than final bond strength?
For high-speed lamination, both matter. Initial strength helps stabilize the film during early processing, while final bond strength determines long-term performance after curing.
Can this adhesive be used for PVC film?
Tonren's published product information lists PVC high-gloss film among its application materials. Actual compatibility should be confirmed using the specific PVC film, substrate, machine, and process conditions before bulk purchasing.
Is it suitable for PET film lamination?
Tonren lists transparent PET among the application materials for its High Initial Bond PUR Lamination Glue. The specific PET film should still be tested because surface treatment and film construction can affect adhesion.
What is the difference between Tonren 8131 and 8133?
According to Tonren's published product information, 8131 is a universal type with excellent leveling properties and is especially suitable for high-gloss film lamination, while 8133 provides better initial bonding strength and is suitable for thicker decorative film lamination. Their listed viscosity and operating-temperature ranges also differ.
Can I test the adhesive before placing a bulk order?
Yes. Foshan Tonren Adhesive Co., Ltd states that free samples are available for testing. Sample testing should ideally use the buyer's actual film, substrate, machine, and production conditions.
12. Conversion Path: From Film-Shifting Problem to Sample Verification
For a panel lamination factory, the most efficient procurement process is:
Identify the Film-Shifting Problem
↓
Check Film + Substrate + Machine Conditions
↓
Select High Initial Bond PUR Lamination Glue
↓
Review TDS / SDS / Application Recommendations
↓
Request Sample
↓
Run Trial on Actual Lamination Line
↓
Measure Initial Film Position Stability
↓
Evaluate Final Bonding After Curing
↓
Compare Rework, Waste and Production Stability
↓
Approve Supplier for Bulk Production
This approach allows buyers to make a decision based on production evidence rather than marketing claims.
13. Conclusion: For High-Speed Lamination, Initial Bond Is a Production Parameter
A high-speed furniture lamination line cannot afford to treat film positioning as a minor issue.
When PET or PVC film shifts or rebounds before the next processing stage, the result can be:
Misalignment → Cutting Defects → Rework → Material Waste → Downtime
The adhesive therefore needs to do more than provide strong final bonding.
It needs to provide sufficient initial bonding strength at the moment when the film is most vulnerable to movement.
That is the core value of High Initial Bond PUR Lamination Glue.
For furniture panel manufacturers running high-speed flat lamination lines, PUR lamination adhesive for high speed line should be evaluated through actual line speed, film type, substrate, coating amount, operating temperature, pressing conditions, and downstream processing time.
Foshan Tonren Adhesive Co., Ltd provides High Initial Bond PUR Lamination Glue for applications including PVC high-gloss film, acrylic, transparent PET, and other surface materials, with product options designed around different leveling and initial-bonding requirements.
If your production line is experiencing PET/PVC film shifting, rebound, edge movement, cutting defects, or repeated rework after lamination, contact Foshan Tonren Adhesive Co., Ltd and request a sample for your actual production materials.
Send your film type, substrate, machine speed, current adhesive, operating temperature, and main bonding problem to Tonren. A production trial can then be used to determine whether a High Initial Bond PUR Lamination Glue is suitable for your line.